

OTL-60 Coffee Roaster
Full Circulation Industrial Roasting System - OTL 60kg Coffee Roaster
Overview
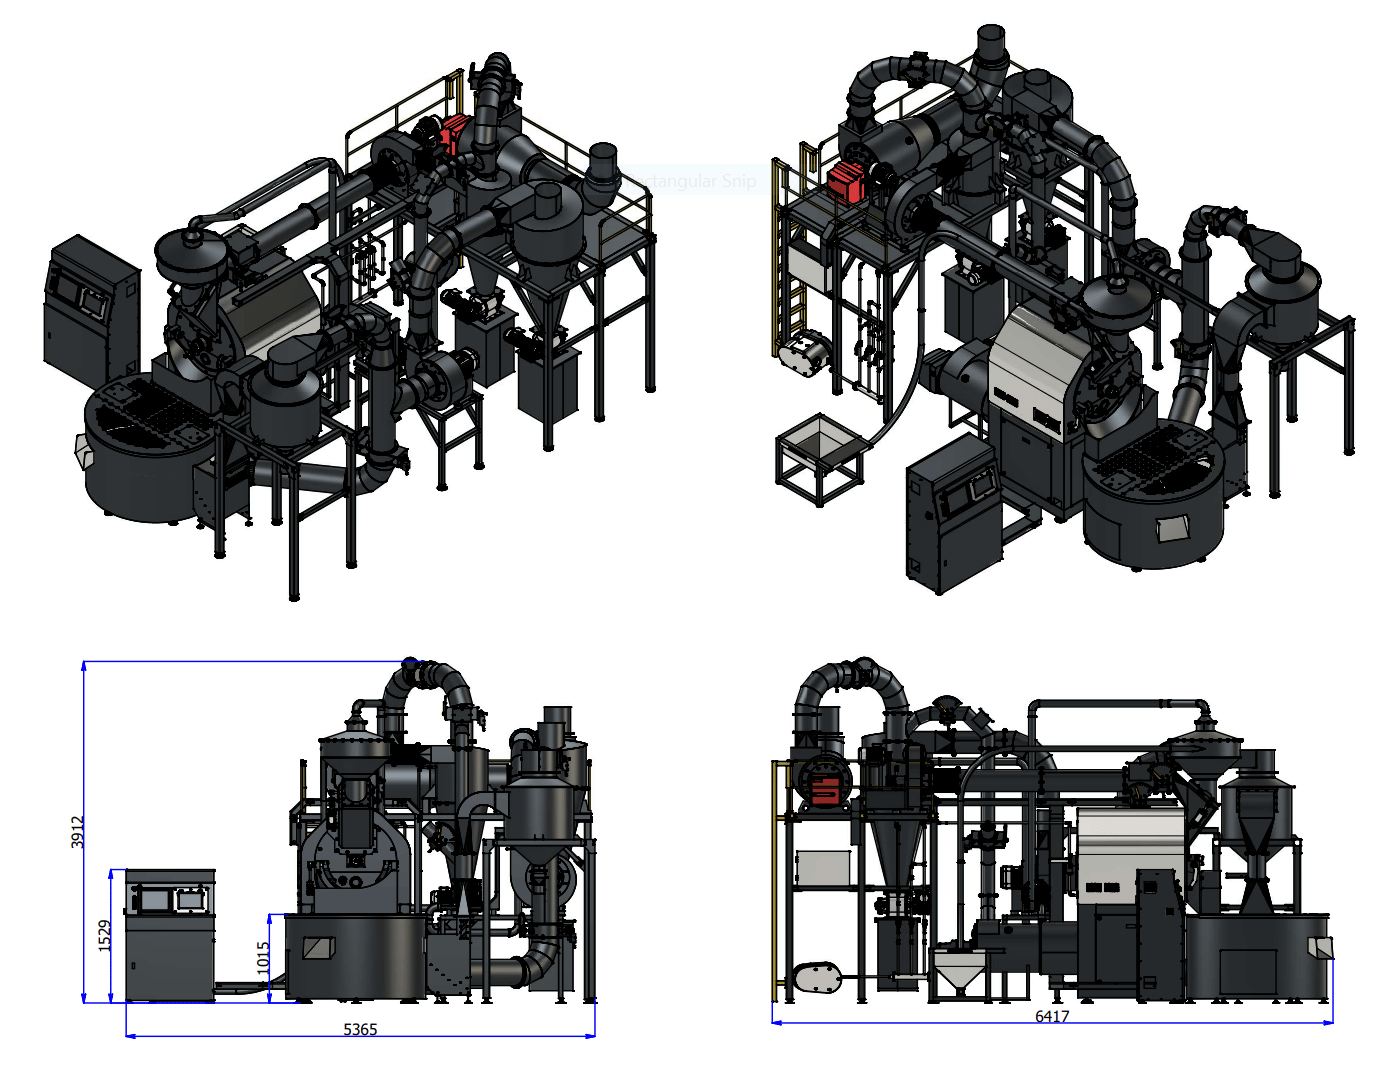
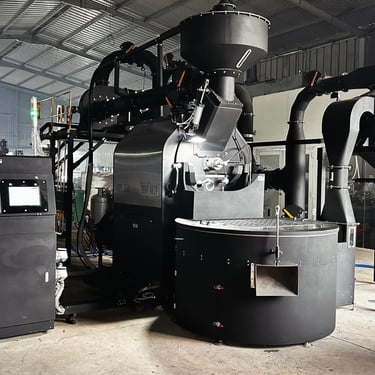
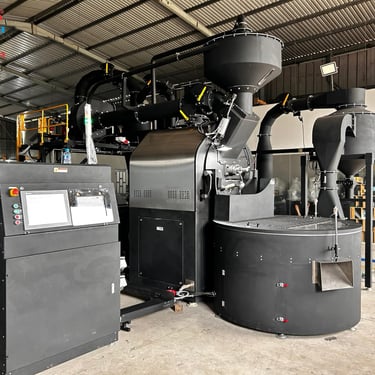
The OTL 60kg Coffee Roaster is a pinnacle of industrial coffee roasting technology. Designed with an advanced full-circulation airflow system, it offers unmatched efficiency, precision, and environmental responsibility. This model is engineered to meet the demands of large-scale production facilities while maintaining superior control over the roasting process.
Specifications
Batch size: 30–60 kg
Output: 180–240 kg/h
Roast time per batch: 12–20 min
Total electrical power: 12 kW
Power supply: 3-phase 380–400 V, 50 Hz
Burner: Weishaupt (Germany), modulating
Dimensions (L × W × H): 6417 × 5365 × 3912 mm
Features:
Full Circulation Airflow System:
Utilizes a closed-loop system to minimize energy waste.
Ensures consistent heat distribution for uniform roasting.
Reduces environmental impact by recycling exhaust air.
Advanced Temperature Control:
Monitors seven critical points: Bean Temperature, Exhaust Temperature, Cooling Temperature, Burner Air Temperature, Chamber Temperature, Cyclone Temperature, and Afterburner Temperature.
Enables precise adjustments to optimize roast profiles.
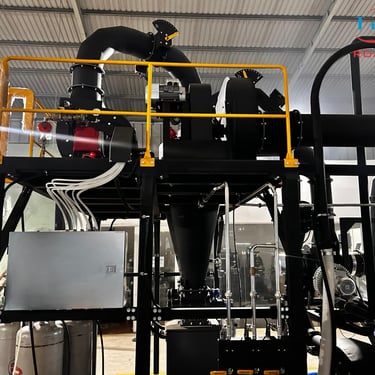
High-Efficiency Afterburner:
Integrated afterburner ensures clean emissions.
Afterburner chamber up to 600 °C for treating roasting smoke and odour.
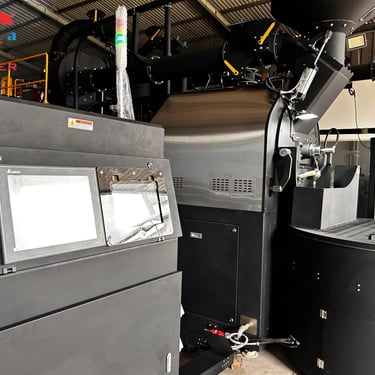
Touchscreen Control Panel:
User-friendly interface with real-time data monitoring.
Programmable roasting profiles for consistent results across batches.
Robust Construction:
Made with high-grade materials to ensure durability.
Modular design simplifies maintenance and upgrades.
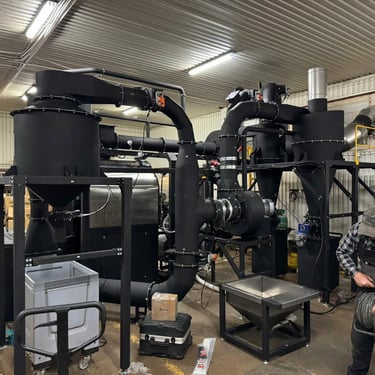
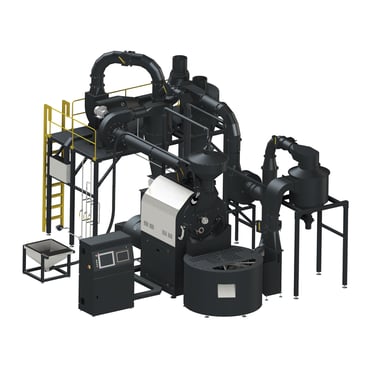
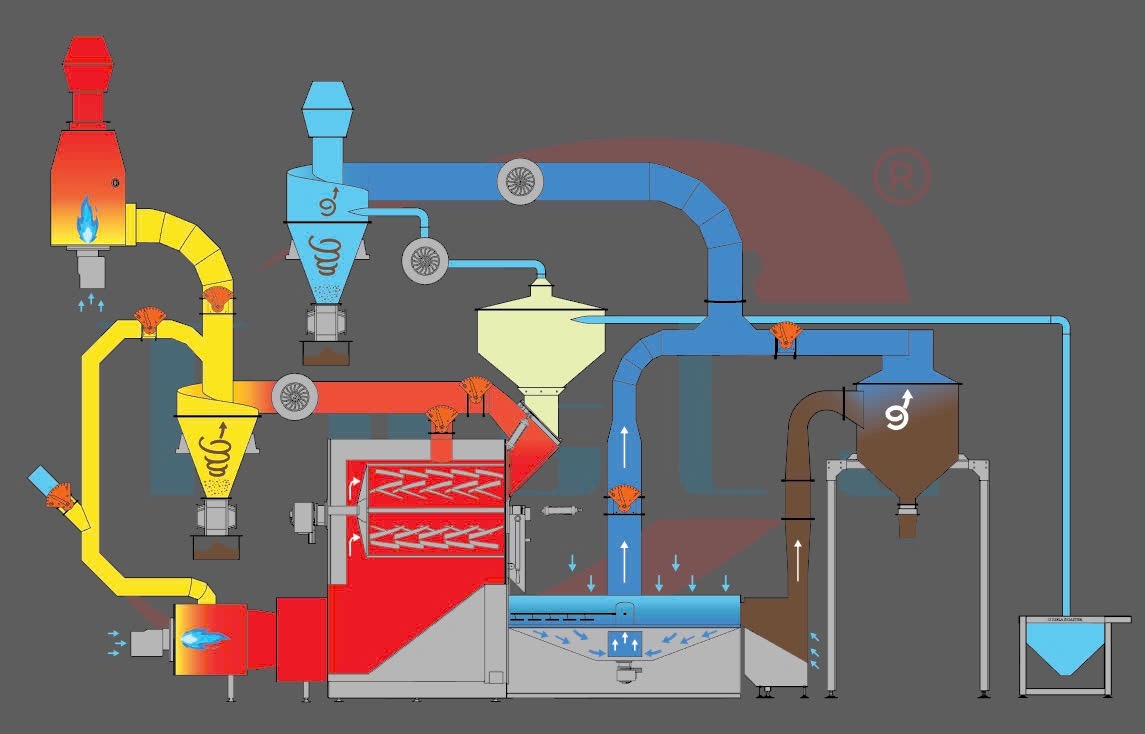
System Diagram Explanation:
Bean Temp: Tracks the coffee beans' core temperature for precision roasting.
Exhaust Temp: Manages airflow and ensures the system remains clean and efficient.
Cooling Temp: Rapidly cools roasted beans to preserve flavor and prevent over-roasting.
Burner Air Temp & Chamber Temp: Ensures optimal heat delivery and consistency.
Cyclone Temp: Collects chaff and ensures efficient air circulation.
Afterburner Temp: Final stage for cleaning exhaust gases and reducing pollutants.
Applications:
Ideal for industrial-scale coffee production facilities.
Suitable for roasters focusing on sustainable practices and high-quality output.
Benefits:
Heat recovery reduces gas consumption by 15–20% (design value).
Maintains product quality at scale with precise and consistent roasting.
Supports environmental goals with low emissions and energy-efficient technology.